Unlocking Efficiency: The Wonders of an Optical Sorting Machine
2026-03-04


Image Source: unsplash
Introduction: The Magic of Optical Sorting
Have you ever wondered how food manufacturers ensure their products are free from unwanted materials? Well, look no further than the optical sorting machine! These ingenious devices employ cutting-edge technology to sift through materials at lightning speed, making them essential in various industries.
What is an Optical Sorting Machine?
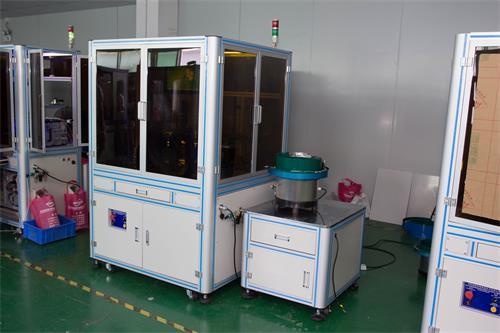
In simple terms, an optical sorting machine is a device that uses cameras and sensors to identify and separate items based on color, shape, or size. Think of it as a high-tech version of the classic sorting hat from Harry Potter, but instead of determining your Hogwarts house, it sorts everything from grains to fruits!
How Does It Work?
So, how does this amazing contraption do its thing? Basically, it works by illuminating the items on a conveyor belt with LED lights. As items pass through, cameras capture images and analyze the data. If an item doesn't meet the required specifications, it gets blasted away by high-speed air jets, ensuring only the best products make it through.
Benefits of Using Optical Sorting Machines
Now, let's get down to the nitty-gritty. Why should businesses consider using an optical sorting machine? Here are a few compelling reasons:
- Increased Efficiency: These machines can process thousands of items per hour, saving time and boosting productivity.
- Improved Quality: By removing defective items, companies can ensure that their final products meet high standards.
- Cost Savings: Although the initial investment may be substantial, the long-term savings from reduced manual labor and waste are significant.
Applications Across Industries
From agriculture to recycling, optical sorting machines have found their place in various sectors:
- Agriculture: Farmers use these machines to sort fruits, vegetables, and nuts, ensuring only the finest reach grocery stores.
- Food Processing: In food factories, they help in separating good grains from bad, enhancing product safety.
- Recycling: They are pivotal in sorting plastics and metals, fostering a greener planet by improving recycling rates.
Challenges and Considerations
Of course, it's not all sunshine and rainbows. Like any technology, there are challenges:
- Initial Costs: The price tag can be a hurdle for smaller businesses, but the ROI often makes it worthwhile.
- Maintenance: Regular upkeep is necessary to keep these machines running smoothly, which can add to operational costs.
Future Trends in Optical Sorting
As technology continues to evolve, so do optical sorting machines. Innovations like AI integration and machine learning are on the horizon, promising even smarter and more efficient sorting capabilities. Imagine a machine that learns from its mistakes, continually improving its sorting accuracy—now that's a game-changer!
Conclusion: A Bright Future Ahead
In conclusion, the optical sorting machine is not just a fancy gadget; it's a powerhouse of efficiency and accuracy. As industries strive for higher quality and lower waste, these machines are proving to be invaluable. If you're looking to boost your operations, investing in this technology might just be the ticket!
Related News
Contact Us
Ms. Lu: +86-18128878019
Phone: +86 0755-23199519
ADD : Room 302, 402, Building A, Xinpitou Industrial Zone, Kanghong Road, Xinqiang Community, Xinhu Street, Guangming New District, Shenzhen
Online Message
Our team will get in touch with you shortly, so keep an eye on your inbox