

Unlocking Efficiency: The Role of Magnetic Ring Core Optical Sorting Machines in Material Processing
2025-11-28


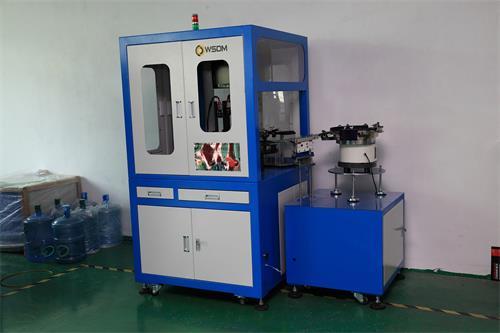
In the manufacturing and processing sector, the efficiency of sorting and screening machinery can significantly impact overall productivity and material quality. One innovative solution that has gained traction is the Magnetic Ring Core Optical Sorting Machine. This advanced technology employs optical sensors and magnetic principles to enhance the sorting process of various materials, ensuring a higher level of accuracy and effectiveness in separating different material types.
A Magnetic Ring Core Optical Sorting Machine operates by using a combination of advanced imaging technology and powerful magnetic fields. This dual approach allows the machine to detect and differentiate materials based on their optical and magnetic properties. For example, materials that contain ferrous or non-ferrous elements can be sorted with precision, improving the yield of valuable resources and reducing contamination in the final product.
One of the primary advantages of utilizing a Magnetic Ring Core Optical Sorting Machine is its ability to significantly increase sorting speed. Traditional sorting methods can be labor-intensive and time-consuming, often leading to bottlenecks in production. In contrast, these optical sorting machines can process large quantities of material rapidly, allowing manufacturers to maintain a continuous workflow and meet production demands more effectively.
Moreover, the integration of optical technology enables the machine to identify a broader range of materials than conventional sorting systems. This capability is particularly beneficial in industries where diverse material types are processed, such as recycling and mineral processing. By accurately identifying and sorting materials, companies can enhance their operational efficiency and minimize waste, further contributing to sustainability efforts.
Another critical feature of the Magnetic Ring Core Optical Sorting Machine is its adaptability. These machines can be customized to cater to specific sorting requirements based on the materials being handled. Whether it’s sorting plastics, metals, or other composites, the flexibility of this system ensures that businesses can optimize their processes for various applications.
In conclusion, Magnetic Ring Core Optical Sorting Machines represent a significant advancement in the field of sorting and screening machinery. By leveraging cutting-edge technology, businesses can enhance their operational efficiency, improve sorting accuracy, and adapt to a variety of material processing needs. As industries continue to evolve, investing in such innovative equipment will be crucial for maintaining a competitive edge and meeting the demands of a changing marketplace.
A Magnetic Ring Core Optical Sorting Machine operates by using a combination of advanced imaging technology and powerful magnetic fields. This dual approach allows the machine to detect and differentiate materials based on their optical and magnetic properties. For example, materials that contain ferrous or non-ferrous elements can be sorted with precision, improving the yield of valuable resources and reducing contamination in the final product.
One of the primary advantages of utilizing a Magnetic Ring Core Optical Sorting Machine is its ability to significantly increase sorting speed. Traditional sorting methods can be labor-intensive and time-consuming, often leading to bottlenecks in production. In contrast, these optical sorting machines can process large quantities of material rapidly, allowing manufacturers to maintain a continuous workflow and meet production demands more effectively.
Moreover, the integration of optical technology enables the machine to identify a broader range of materials than conventional sorting systems. This capability is particularly beneficial in industries where diverse material types are processed, such as recycling and mineral processing. By accurately identifying and sorting materials, companies can enhance their operational efficiency and minimize waste, further contributing to sustainability efforts.
Another critical feature of the Magnetic Ring Core Optical Sorting Machine is its adaptability. These machines can be customized to cater to specific sorting requirements based on the materials being handled. Whether it’s sorting plastics, metals, or other composites, the flexibility of this system ensures that businesses can optimize their processes for various applications.
In conclusion, Magnetic Ring Core Optical Sorting Machines represent a significant advancement in the field of sorting and screening machinery. By leveraging cutting-edge technology, businesses can enhance their operational efficiency, improve sorting accuracy, and adapt to a variety of material processing needs. As industries continue to evolve, investing in such innovative equipment will be crucial for maintaining a competitive edge and meeting the demands of a changing marketplace.
Contact Us
Ms. Lu: +86-18128878019
Phone: +86 0755-23199519
ADD : Room 302, 402, Building A, Xinpitou Industrial Zone, Kanghong Road, Xinqiang Community, Xinhu Street, Guangming New District, Shenzhen
Online Message
Our team will get in touch with you shortly, so keep an eye on your inbox




