

Unlocking Efficiency: The Role of screening machines in Modern Industries
2025-01-02


Unlocking Efficiency: The Role of screening machines in Modern Industries
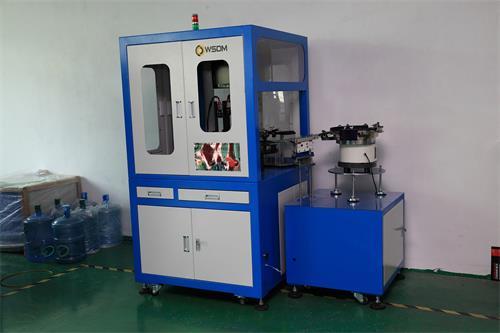
In today's fast-paced world, industries are constantly on the lookout for ways to improve efficiency and output. Enter the screening machine—a pivotal player in the realm of industrial processes. But what exactly are these machines, and why are they considered essential?
What is a screening machine?
To put it simply, a screening machine is designed to separate materials based on size and other characteristics. Think of it as a highly efficient sieve, sorting out the good from the bad. Whether it’s in the food industry, mining, or recycling, these machines are everywhere, working tirelessly behind the scenes.
The Nuts and Bolts: How Do They Work?
Let’s break it down. Most screening machines utilize a series of vibrating screens that allow particles to pass through while retaining larger materials. This process not only speeds up production but also ensures a higher quality of output. For instance, in the construction industry, using a screening machine to sift through aggregates can drastically reduce waste and improve material quality.
Benefits Galore!
So, why should industries invest in a screening machine? Here’s the lowdown:
- Increased Efficiency: These machines can process large volumes of material swiftly, ensuring that companies can meet tight deadlines without breaking a sweat.
- Cost-Effective: By reducing waste and improving material quality, screening machines can lead to significant cost savings in the long run.
- Quality Control: They help ensure that the final product meets industry standards by effectively removing impurities or undesired materials.
- Versatility: Screening machines can be tailored to various industries, from pharmaceuticals to agriculture.
Industry Applications: A Closer Look
Now, let’s take a peek at how different sectors leverage screening machines:
1. Mining and Aggregates
In the mining sector, the efficiency of a screening machine can mean the difference between profit and loss. These machines help in classifying ores, ensuring that only the best materials are processed further. It’s like having a quality control inspector right in the heart of the operation!
2. Food Processing
When it comes to food safety, screening machines play a crucial role. They help in removing foreign materials from grains, ensuring that what reaches consumers is safe and clean. Talk about peace of mind!
3. Recycling
The recycling industry has also embraced screening machines, using them to separate different materials for processing. This not only promotes sustainability but also maximizes the efficiency of recycling operations.
Choosing the Right screening machine
Now, you might be wondering how to choose the right screening machine for your needs. Here are some tips:
- Know Your Materials: Different materials require different types of screening processes. Be clear about what you’ll be screening.
- Consider Capacity: Make sure to select a machine that can handle your production volume without a hitch.
- Look for Customization Options: Some providers offer machines that can be tailored to meet specific industry needs.
Future Trends in Screening Technology
As technology advances, so do screening machines. New innovations, such as automated systems and AI integration, are on the horizon. Imagine a future where screening machines not only separate materials but also analyze them for quality, all in real-time! Exciting, right?
Final Thoughts
In conclusion, the screening machine is more than just a tool; it’s a game-changer for many industries. Understanding its functionality and benefits can help businesses make informed decisions that boost productivity and profitability. So, if you’re in the market for a way to enhance your operations, it might just be time to consider investing in one of these machines. You won’t regret it!
Contact Us
Ms. Lu: +86-18128878019
Phone: +86 0755-23199519
ADD : Room 302, 402, Building A, Xinpitou Industrial Zone, Kanghong Road, Xinqiang Community, Xinhu Street, Guangming New District, Shenzhen
Online Message
Our team will get in touch with you shortly, so keep an eye on your inbox




